Industrial chemical specifications can look reassuringly precise while still leaving a buyer exposed. A purity percentage, pH range, or moisture limit may appear decisive, yet those numbers have little value unless they reflect the intended process, a defined test method, and the batch that will actually arrive.
Before issuing a purchase order, buyers should read chemical specifications as a connected technical record. The real question is whether a chemical’s composition, behavior, documentation, and packaging suit the customer’s equipment and end use.
Industrial Chemical Specifications Need More Than Purity
Purity is often the first number buyers compare, but it is rarely the only one that controls performance. A material can satisfy its assay and still create problems because of moisture, insoluble matter, residual solvents, trace metals, particle size, or another application-sensitive impurity.
The useful specification starts with identity, grade, concentration basis, and physical form. Buyers also need to know whether assay is reported as received, on a dry basis, as an active component, or after correction for a volatile fraction.
A high assay does not automatically mean a better process result. Controlled secondary properties may matter as much as nominal purity, so procurement teams should define which characteristics are critical to quality before comparing suppliers.
Assay and Impurities Define the Real Grade
An assay states how much target substance is present, but an impurity profile explains what occupies the remainder. That difference can determine corrosion risk, color, odor, reactivity, catalyst performance, regulatory suitability, and final-product stability.
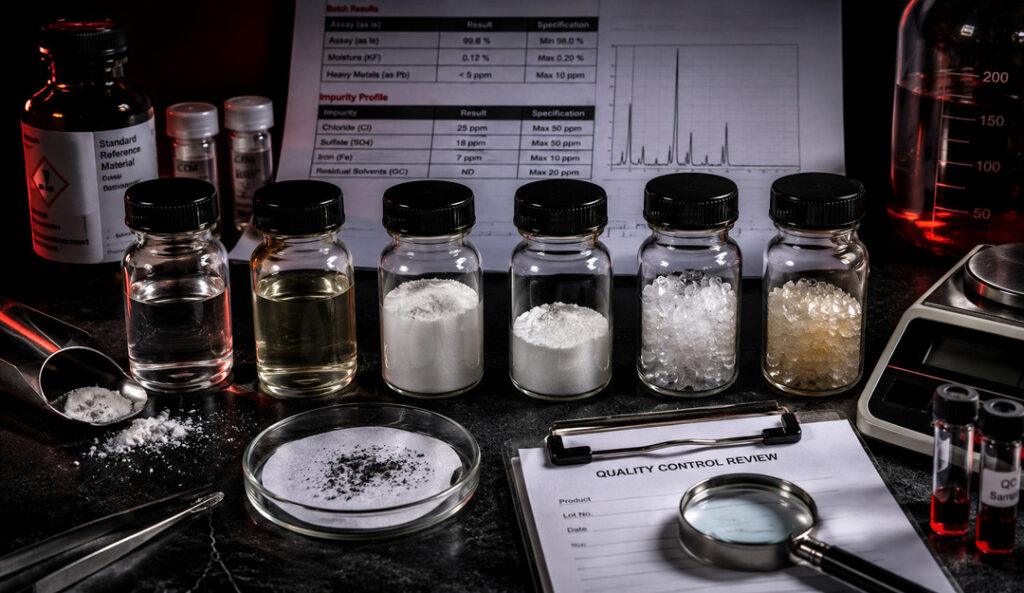
Buyers should review named impurity limits rather than relying on “meets industrial grade.” Relevant limits may include heavy metals, chloride, sulfate, iron, residual solvents, unreacted raw materials, ash, water, or insoluble matter.
A specification also needs clear acceptance limits. “Typical” values describe expected performance but may not create a firm release requirement. Minimums, maximums, and defined ranges are more useful because they establish what can be accepted or rejected.
| Data Point | What It Can Affect | Question to Ask |
|---|---|---|
| Assay or active content | Dose, yield, formulation balance | What reporting basis and method are used? |
| Moisture or loss on drying | Stability, flow, dilution, storage | When and how is it measured? |
| Trace impurities | Color, corrosion, toxicity, side reactions | Which impurities have individual limits? |
| Particle size | Dispersion, filtration, settling | Is the result an average or distribution? |
| pH or acidity | Compatibility and reaction behavior | What concentration and temperature are used? |
| Bulk density or specific gravity | Dosing, storage, freight, mixing | How is the value determined? |
The table is a starting screen, not a universal checklist. The buyer’s process should decide which limits become contractual, because the same chemical may require different controls in different plants.
Physical Properties Determine Whether the Material Will Run
Chemical composition does not describe how a material will move through production. Powders with similar assay may feed differently because of bulk density, particle-size distribution, shape, surface treatment, moisture, or agglomeration. Liquids may require different pumps, seals, storage temperatures, or mixing conditions because of viscosity, specific gravity, freezing point, or vapor pressure.
Particle-size data deserves attention. A single average can hide fines or oversized particles that affect dust, filtration, dissolution, abrasion, or settling. Buyers should identify whether the supplier reports a median, full distribution, sieve result, or another measurement.
Values such as pH also require context. The result may depend on sample concentration, solvent, temperature, preparation time, and electrode procedure. A pH number without those conditions is difficult to reproduce and may lead to false comparisons.
For hazardous chemicals, the safety data sheet provides standardized safety information, including physical and chemical properties in Section 9. The OSHA safety data sheet requirements show the range of properties that may be reported. An SDS is not a substitute for a product specification because its central purpose is hazard communication rather than performance control.
Test Methods Turn Numbers Into Comparable Evidence
A specification value is incomplete without a test method. Different methods can produce different results because they use different sample preparation, instruments, detection limits, calibration materials, calculations, and endpoints.
Moisture might be measured by oven loss, Karl Fischer titration, or another validated procedure. Particle size may come from laser diffraction, microscopy, sedimentation, or sieving. Assay may be determined by titration, chromatography, spectroscopy, gravimetry, or an application-specific method. Results are not interchangeable merely because they share the same unit.
Buyers should request the method, sample preparation, reporting basis, and tolerance. They should also determine whether it is a recognized standard, modified standard, or supplier method. An internal procedure must still support repeatability and dispute resolution.
Measurement traceability deserves attention when narrow limits or expensive failures are involved. NIST explains that metrological traceability connects a result to a stated reference through a documented chain of calibrations, with each link contributing to uncertainty. A decimal place is not proof of accuracy. The laboratory system must support the precision reported.
Documents Must Follow the Actual Batch
The technical data sheet describes general characteristics, while the certificate of analysis reports results for a specific batch. The safety data sheet addresses hazards and safe handling. Regulatory declarations and certificates of conformity answer different questions.
These documents should agree on identity, grade, concentration, and limits. A certificate of analysis should connect to the delivery through the product name, lot number, test results, limits, and approval status.
Buyers should be cautious when every certificate reports the same “typical” values, results contain more precision than the method supports, or the certificate lists only pass/fail outcomes for characteristics that need trend analysis. Repeated identical results may indicate that actual batch data is not being disclosed.
Document control is part of product control. Current revisions should be available before approval, and obsolete specifications should not remain active in purchasing systems. Incoming inspection plans, purchase descriptions, and supplier agreements should refer to the same approved requirements.
Supplier Changes That Should Stop an Automatic Reorder
The greatest technical risk may appear after a chemical has performed well for years. A supplier can change a raw-material source, manufacturing site, process condition, test method, packaging component, specification range, or subcontract laboratory without changing the commercial name.
Those changes can shift impurity patterns, particle behavior, color, odor, moisture pickup, or analytical comparability. Procurement and quality teams should define which changes require advance notice, document review, samples, plant trials, or requalification.
Warning signals include wider variation, unexplained certificate revisions, missing impurity results, packaging substitutions, handling problems, or complaints concentrated around particular lots. Trend data can reveal deterioration before a batch crosses a limit.
The right purchasing decision combines specification review with supplier capability. Buyers should confirm change control, batch traceability, laboratory competence, and the ability to explain unusual results.
Industrial chemical specifications work when they translate a process into measurable requirements. The goal is not to collect the longest data sheet or demand the highest purity. It is to identify the properties that control performance, verify how they are measured, and ensure the delivered batch matches the approved material.
As supply chains change, disciplined review becomes more valuable. A buyer who checks identity, assay basis, impurity limits, physical properties, methods, batch evidence, and change control is better positioned to prevent quality drift before it reaches production.
FAQs
What Are the Most Important Technical Data Points to Check?
Start with the properties that control your process and final product. Assay, impurities, moisture, particle size, pH, density, and viscosity matter only when tied to defined methods and acceptance limits.
Is a Safety Data Sheet Enough to Approve a Chemical?
No. An SDS communicates hazards, handling precautions, and physical or chemical properties. Buyers still need a technical data sheet, approved specification, and batch-specific certificate of analysis to evaluate quality and performance.
When Should an Industrial Chemical Be Requalified?
Review or requalify the material after changes to raw-material sources, manufacturing sites, production processes, test methods, specification limits, packaging, or laboratories, especially when those changes could affect performance.