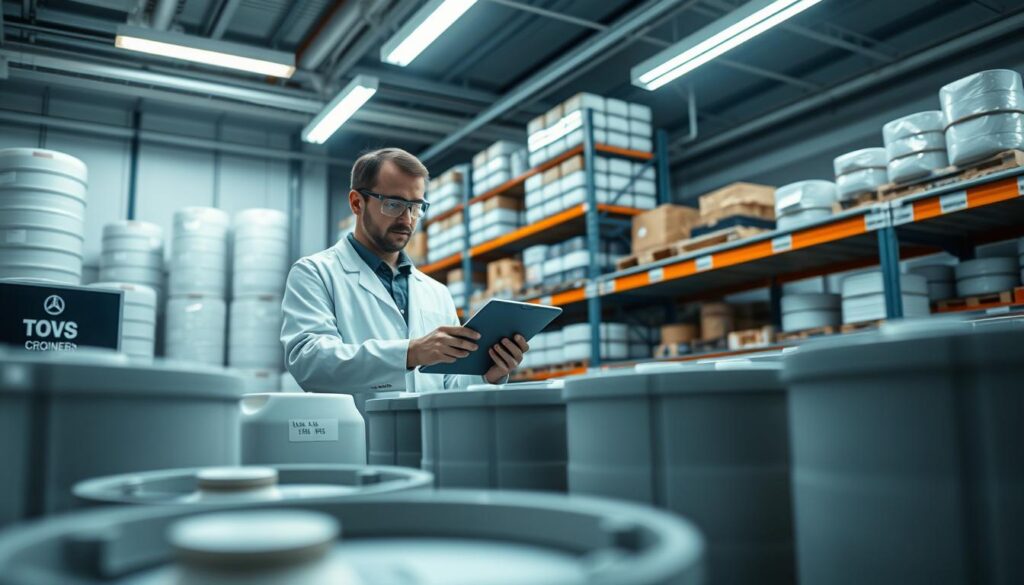
Choosing the right container is your first and most critical step toward product stability. This decision sets the foundation for everything that follows, from safe transport to long-term storage.
You have powerful options. Steel and polyethylene drums offer robust protection. Intermediate Bulk Containers (IBCs) provide versatile, large-scale solutions. Systems like bag-in-box add a layer of convenience and safety. This decision also supports impurity control for industrial chemicals across the full product handling cycle.
Your product’s unique properties guide this choice. Is it a thin liquid or a thick gel? Is it sensitive to oxygen or highly reactive? The answers point you toward specialized liners—like EVOH barriers—and specific filling methods.
Never underestimate the closure. Proper vented caps are essential for many products. They maintain a safe pressure balance inside the container, which directly protects your product’s integrity.
Mastering these fundamentals empowers you. You’ll confidently select the combination that best preserves your product’s quality and extends its shelf life from day one.
Permeation and swell: when polymers fail and how to read charts/data
When polymers fail, it’s often due to permeation—the silent migration of molecules—or swell, the visible deformation of plastic. These two processes are the primary ways your chemical packaging can lose its battle to contain your product. Understanding them is your first line of defense against spoilage, loss, and safety risks.
Permeation is a slow, molecular-level process. Chemical molecules from your product gradually work their way through the microscopic pores of the container wall. Think of it like water vapor moving through a Gore-Tex jacket. It doesn’t cause a leak you can see, but it leads to product loss and possible contamination.
A classic failure from permeation is called paneling. During an accelerated aging test—like storing a bottle for 14 days at 140°F—an incompatible chemical can leach out through the plastic. This creates a vacuum inside the container, causing the walls to buckle inward. If you see a collapsed or deformed bottle, permeation is often the culprit.
Swell is the physical expansion or softening of the polymer material itself. The chemical is absorbed into the plastic, causing it to increase in volume and lose its structural strength. A swollen drum or Intermediate Bulk Container (IBC) can become difficult to handle and may even rupture.
So, how do you predict these interactions before filling a thousand containers? You rely on chemical compatibility charts and supplier data. These tools are not just simple “yes/no” lists. They provide critical data on permeation rates and swell percentages over time.
Here’s how to read them effectively:
Start with the Safety Data Sheet (SDS): Review Section 10, “Stability and Reactivity.” It lists materials to avoid and can hint at possible compatibility issues.
Find the Right Chart: Locate a compatibility chart specific to your container resin (e.g., HDPE, PP) and your chemical. Reputable suppliers provide these.
Interpret the Ratings: Look for codes or ratings beyond just “A” (Excellent) or “B” (Good). Pay close attention to any footnotes about long-term exposure or elevated temperature effects.
Analyze the Data: Some advanced charts show weight change percentages (indicating swell) or transmission rates (indicating permeation) after specific time intervals. A low permeation rate is your goal.
Accelerated aging test data is gold. A test that shows no paneling, negligible weight change, and maintained clarity after aggressive conditions gives you high confidence for real-world storage. This data helps you select resins that act as a robust barrier, preserving your product’s purity and potency.
Don’t guess with your valuable materials. A small investment in reviewing compatibility data prevents the huge cost of product loss, failed stability tests, and damaged customer trust. Master reading these charts, and you turn packaging from a simple container into a guaranteed shield.
Storage conditions: temperature/humidity, light/UV, venting/blanketing, headspace control
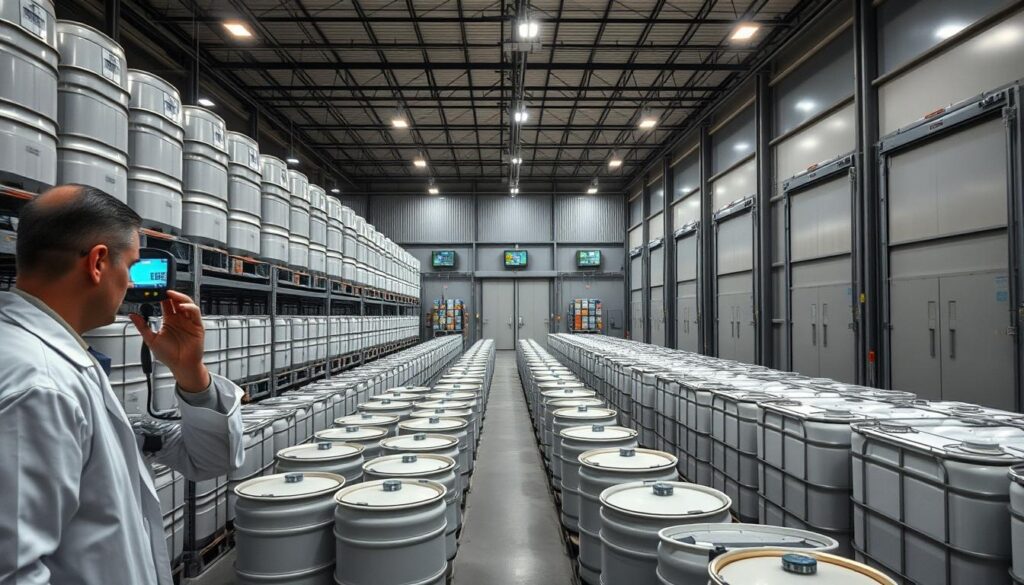
Your warehouse or storage area is more than a holding space. It acts as the primary guardian of your product’s shelf life. Here, mastering environmental variables directly translates to preserved quality and value. This guide focuses on the four pillars you can control: temperature and humidity, light exposure, venting or blanketing, and headspace management.
Think of these factors as your stability toolkit. Proper management is a core stewardship activity, ensuring both packaging and product integrity from the moment of receipt.
Temperature and Humidity: The Dynamic Duo
Consistent temperature control is non-negotiable for sensitive chemicals and ingredients. Fluctuations accelerate degradation reactions. Your first step is to identify the ideal storage range for your specific materials.
Use continuous data loggers to monitor conditions. Don’t just check the thermostat. Track the actual ambient temperature where drums or IBCs are stored.
Humidity plays a supporting yet critical role. High humidity can promote corrosion on metal containers or cause labels to degrade. It can also affect certain polymer liners. Aim for a stable, moderate humidity range, typically between 40% and 60% RH.
For long-term storage or transport through variable climates, consider the packaging itself. UV-protected and multi-layer barrier liners inside containers add a vital defense layer against external temperature and moisture swings.
Sunlight and artificial light are silent aggressors. Ultraviolet (UV) radiation breaks down chemical bonds, leading to discoloration, potency loss, and formation of unwanted by-products.
Your mitigation strategy should be multi-layered:
- Store all containers away from windows and direct light sources.
- Use opaque or light-blocking secondary packaging.
- Choose containers or liners with built-in UV inhibitors.
- Apply UV-blocking films to warehouse windows.
This proactive light management is a simple, highly effective step in your stability playbook.
Venting, Blanketing, and Headspace: Controlling the Atmosphere
The air inside your container is just as important as the environment outside. Here, you have two main strategies: venting and inert gas blanketing.
Venting allows containers to “breathe,” equalizing pressure during temperature changes. This prevents bulging or collapse. But, it also allows moist or oxygen-rich air to enter.
For oxygen-sensitive products, nitrogen blanketing is the gold standard. By displacing the air in the headspace with inert nitrogen, you create a protective atmosphere that drastically slows oxidation.
Headspace control is critical. It’s not just empty volume. A minimal, well-managed headspace limits the amount of oxygen available to react with your product. This is essential for maintaining the concentration of volatile inhibitors. A large, air-filled headspace can lead to rapid inhibitor depletion and product instability.
| Storage Factor | Ideal Condition | Common Risk | Primary Mitigation Strategy |
|---|---|---|---|
| Temperature | Product-specific stable range (e.g., 15-25°C) | Thermal degradation, accelerated reactions | Climate-controlled area with continuous monitoring |
| Humidity | 40-60% Relative Humidity | Corrosion, label damage, moisture ingress | Dehumidifiers, sealed barrier packaging |
| Light / UV | Complete darkness or UV-filtered light | Photo-degradation, color change | Opaque storage, UV-blocking containers/films |
| Headspace Atmosphere | Inert (Nitrogen) or Dry Air | Oxidation, moisture contamination, pressure change | Nitrogen blanketing systems, sealed liners, proper venting |
By taking command of these storage conditions, you build a powerful, proactive defense. You move from simply storing materials to actively preserving them. This disciplined approach to temperature control and environmental management forms the unshakable foundation of your product stability strategy.
Inhibitors/stabilizers: tracking ppm, safe sampling, top‑up criteria
The Safety Data Sheet (SDS) is more than just a rulebook. It’s your guide to managing the chemicals in your products. A detailed SDS review shows you the active ingredients. This info is key for any inhibitor monitoring plan.
These additives are used in tiny amounts. It’s important to track their ppm levels. You need to set a baseline ppm when you first get the product. Then, test regularly to see if levels change.
Levels can drop due to evaporation, reactions, or absorption. A steady decrease in ppm means protection is weakening. Without this info, you’re managing in the dark.
To get this data, you need to sample safely. Contamination can ruin your batch and mess up your results. Here are the main steps for clean sampling:
- Use dedicated, clean sampling tools for each product or inhibitor type.
- Sample from a well-mixed, representative portion of the container.
- Perform sampling in a controlled environment to minimize exposure to air, moisture, or light.
- Label samples immediately with date, time, batch number, and sampler ID.
This careful method ensures your ppm readings are right. Right readings mean you know when to act. You need clear rules for adding more inhibitors.
Adding more isn’t a guess. It’s based on your ppm data and the product’s stability. The table below shows what to look for.
| Parameter | Target Range | Monitoring Frequency | Action Trigger |
|---|---|---|---|
| Inhibitor PPM Level | As specified on SDS (e.g., 50-150 ppm) | Quarterly or per shelf-life check | Level falls below 10% of lower spec limit |
| Product Viscosity Change | ±5% from baseline | At each sampling event | Change exceeds 5%, correlates with ppm drop |
| Color or Clarity | No change from standard | Visual check at each sampling | Any visible cloudiness or color shift |
| Acid Number / pH | Within manufacturer range | With every ppm test | Shift indicates active degradation |
Use the table’s triggers to make a formal top-up plan. The plan should say what inhibitor to add, how much, and how to mix it. Always add stabilizers slowly and mix well to spread them evenly.
Think of your inhibitor monitoring system as an early warning. It catches problems before they affect quality. This proactive approach saves product, cuts waste, and keeps things consistent.
Mastering ppm tracking, safe sampling, and data-driven top-up rules puts you in control. You turn these silent protectors into reliable allies for long-term storage.
FEFO and inventory controls: barcodes, rotation, retest dates, retains
Imagine an inventory where every item is used at its best quality. This is what a First-Expired, First-Out (FEFO) system does. It turns your storage into a reliable asset.
At the core of effective FEFO is knowing where everything is. Barcodes or RFID tags help track this. Every scan updates the item’s location and important dates instantly.
Physical rotation must match the digital data. A clear procedure is key. Place new items behind older ones. Train your team to pick from the front first.
Managing dates is more than just watching expiration. You also need to track retest dates based on stability studies. Data from packaging certifications is essential. UN performance marks help calculate a container’s safe life and plan rotation.
Key parts of a strong FEFO system include:
- Unique Identification: Every container has a scannable barcode or RFID tag.
- Date Code Management: Systematically log manufacturing, receipt, and retest dates.
- Visual Warehouse Layout: Designated lanes and clear labeling for different product codes.
- Retain Sample Protocol: Pull and securely store samples from each batch for future investigation.
Keeping “retain” samples is a safety measure. If a quality issue comes up, you can analyze the exact batch. This protects your process and gives clear answers.
Strong FEFO controls give you confidence. You know every product is used within its best window. This prevents waste and ensures quality results. Start your system today and make inventory management your advantage.
Transfer to use point: hose/pump compatibility, filtration on transfer, cleanliness classes
Keeping your product quality safe doesn’t stop at the storage drum. The transfer process has its own risks of contamination. This is where all your hard work on stability can be undone. A clean, compatible transfer system is your last defense.
Choosing the right equipment is the first step. Hoses, seals, and pump parts must be chemically compatible. If they’re not, they can leach harmful substances or react with your product, causing quality to degrade over time.
For thick products, how you fill and dispense them is key. Using a bottom-drain liner in an IBC is often the safest and most efficient choice. It minimizes product loss and reduces exposure to air. Always match your transfer setup to your operational needs for both safety and speed.

Material compatibility charts are essential tools. Don’t just guess. Consult them for every component that touches your product. Common pitfalls include using standard rubber hoses with aggressive solvents. Fluoropolymer-lined hoses or stainless-steel pumps are often better choices. This proactive step prevents unseen reactions that shorten effective shelf life.
In-Line Filtration: A Non-Negotiable Best Practice
Installing a filter during transfer is a simple, powerful safeguard. It captures particulates from the container, transfer line, or environment. Even in sealed systems, microscopic debris can be present.
Filtration protects downstream equipment and ensures product purity. Select a filter micron rating based on your product’s sensitivity. For most chemicals, a 10-micron filter is a good start. For ultra-pure applications, you may need sub-micron filtration. Remember to document filter changes as part of your quality records.
Defining Your Cleanliness Class
Not all transfers require the same level of cleanliness. Defining a “cleanliness class” for your operation sets a clear standard. This guides your cleaning procedures and equipment selection.
Your industry and product use dictate the class. A food-grade additive has different requirements than a pharmaceutical intermediate. High-purity electronics chemicals demand the strictest protocols. Establishing this class ensures every transfer supports your product’s intended shelf life.
| Cleanliness Class | Typical Industry | Key Requirements | Example Transfer Equipment |
|---|---|---|---|
| Industrial Standard | General Chemicals, Paints | Visually clean, no gross contamination | Dedicated rubber hoses, centrifugal pumps |
| Food Grade | Food & Beverage, Additives | FDA-approved materials, sanitizable surfaces | White FDA hose, sanitary diaphragm pumps |
| High Purity | Pharmaceuticals, Cosmetics | Validated cleaning, low particle count | 316L stainless steel, PTFE-lined systems |
| Ultra High Purity | Semiconductors, Electronics | Electropolished surfaces, particle-free seals | Perfluoroalkoxy (PFA) tubing, double diaphragm pumps |
Implementing these three pillars—compatibility, filtration, and cleanliness—creates a robust transfer process. It bridges the gap between stable storage and successful use. This disciplined approach removes variables that can unpredictably shorten your product’s shelf life. Your material arrives at the line ready to perform, just as you intended.
Shelf‑life extension case notes and a storage SOP template
Putting theory into practice is the final step. The principles of material compatibility, environmental control, and inhibitor management directly support shelf life extension.
Real-world applications prove the value. A specialty chemical producer switched from standard polyethylene drums to IBCs with a high-barrier liner from Scholle IPN. This change cut permeation losses by over 90%. It added months to the product’s shelf life during bulk storage.
In another case, a pharmaceutical firm faced stability issues with a light-sensitive active ingredient. They adopted nitrogen blanketing for their stainless steel totes. This action minimized oxidative degradation. It allowed for a successful shelf life extension request with regulatory bodies.
To systematize these best practices, a formal Storage Standard Operating Procedure is essential. Our template provides a foundational structure. It guides you in documenting policies for container selection, storage condition monitoring, FEFO inventory rotation, and safe transfer protocols.
Model your SOP on the stewardship seen in reusable packaging management programs. This creates a living document for your team. Consistent adherence to its protocols is the surest way to maximize product shelf life and ensure stability from warehouse to point of use.