A coating manufacturer may achieve an excellent fineness-of-grind result with titanium dioxide, only to discover that the finished paint develops uneven color, reduced gloss or poor storage stability.
The problem may not be inadequate grinding. Pigment particles that were successfully dispersed can come together again after the binder and other formulation ingredients are added.
This process is called titanium dioxide flocculation, and it creates an important distinction for chemical buyers: a pigment’s initial dispersion quality does not guarantee its stability in the finished coating.
Research published in May 2026 provides additional evidence that the interaction between titanium dioxide particles, dispersants and binder materials can affect final coating performance.
For paint manufacturers evaluating alternative titanium dioxide grades, the practical lesson is clear. Qualification should examine what happens after pigment dispersion, not simply whether the initial grinding stage meets its specification.
What Causes Titanium Dioxide Flocculation?
Titanium dioxide (TiO₂, CAS 13463-67-7) is widely used in coatings because it scatters visible light effectively, providing whiteness and hiding power.
However, the pigment particles do not automatically remain evenly separated when incorporated into a liquid formulation.
During grinding, mechanical energy breaks apart pigment agglomerates and distributes the particles through the liquid medium.
The pigment surfaces must then be stabilized to prevent the particles from gathering again.
The specialist manufacturer BYK explains the distinction in its technical overview of pigment dispersion and flocculation. Mechanical dispersion can separate pigment agglomerates, but the resulting particles may subsequently form new clusters.
These newly formed clusters are known as flocculates.
Several factors can influence the process, including particle-surface characteristics, dispersant selection, binder compatibility, pH and interactions with other formulation ingredients.
The result may be a loss of optical performance or a change in the coating’s flow behavior.
Flocculation is not always associated with visible particles or obvious grit.
Some flocculated structures can be disrupted by moderate shear and then reform when the coating is left undisturbed.
This explains why a sample may look improved immediately after stirring but develop problems again during storage.
Initial dispersion is not stability.
A pigment must remain suitably distributed throughout the relevant manufacturing, storage and application conditions.
Why Binder Addition Can Change Pigment Behavior
Industrial coating production often separates pigment incorporation into two stages.
The first is the millbase, where pigments are wetted, dispersed and stabilized using suitable additives and mechanical mixing.
The second is the let-down, where additional binder and other formulation ingredients are incorporated to produce the finished coating.
A pigment can behave acceptably during the first stage but become less stable during the second.
The reason is that adding the binder changes the chemical environment surrounding the particles.
This may affect dispersant adsorption, electrostatic interactions, compatibility and the stability of the pigment suspension.
A 2026 study in the Journal of Coatings Technology and Research investigated functionalized polymer particles as alternatives to conventional titanium dioxide dispersants. The researchers evaluated pigment dispersion alongside optical performance and the water sensitivity of finished films.
The study found that the functionalization of the polymer particles mattered when replacing conventional dispersants.
It also demonstrated meaningful trade-offs.
Some formulations showed improved resistance to water-related effects while displaying less favorable gloss or surface-roughness results.
The research did not establish that one dispersant system is universally superior.
Instead, it reinforced the importance of matching pigment stabilization with the intended binder system and final coating requirements.
The Same Titanium Dioxide Grade Can Perform Differently
Consider a hypothetical manufacturer evaluating one rutile titanium dioxide grade in two waterborne coating formulations.
Both formulations use the same quantity of pigment and achieve acceptable initial dispersion.
However, the binders have different compositions.
One formulation maintains its optical appearance during storage.
The other develops changes in color uniformity and gloss.
This difference would not automatically mean that the supplied titanium dioxide was defective.
The pigment may interact differently with the two binder systems.
The manufacturer must investigate the full formulation before attributing the problem to raw-material quality.
Binder compatibility can change performance even when the initial pigment specification remains unchanged.
Why a Good Hegman Reading Is Not Enough
A Hegman grind gauge is commonly used to evaluate the fineness of dispersion in paints and pigment concentrates.
It helps identify coarse particles and agglomerates remaining in the tested liquid.
However, it does not directly establish whether the pigment will remain stable after additional ingredients are introduced.
The site’s existing guide to Hegman grind gauges versus particle-size measurements explains the difference between checking coarse material in a dispersion and measuring a particle-size distribution.
Flocculation introduces another consideration.
A sample may meet a specified fineness-of-grind requirement before the particles begin to associate again.
A favorable grind reading therefore answers a narrower question than the one that matters for finished-coating stability.
For a manufacturer changing titanium dioxide suppliers, the correct evaluation should distinguish three stages:
- Whether the pigment disperses adequately under the chosen manufacturing conditions.
- Whether that dispersion remains stable after binder addition.
- Whether the finished coating maintains acceptable properties during storage and application.
These are related but separate performance requirements.
A single laboratory value cannot establish all three.
How Rub-Out Testing Helps Detect Pigment Instability
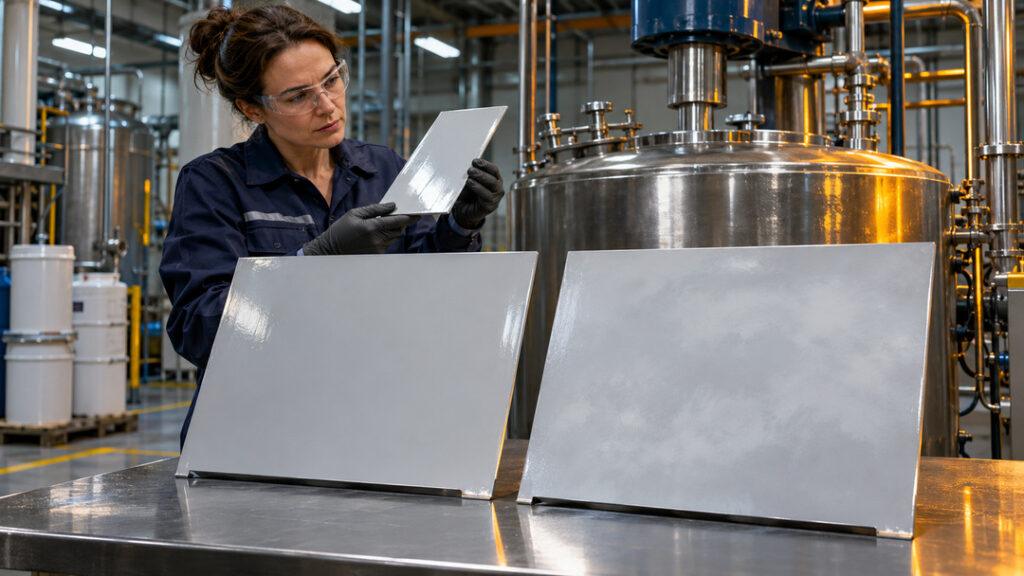
One practical method for investigating pigment instability in tinted coatings is the rub-out, sometimes called a rub-up, test.
This technique examines whether applying additional shear to part of a wet or partially dried coating produces a visible color difference.
The principle is straightforward.
A controlled coating film is applied to a test surface.
A selected area is subjected to additional shear while the film is at the appropriate stage of drying.
The rubbed and unrubbed areas are then compared.
If the pigments are unevenly distributed or poorly stabilized, the extra shear may change their distribution and produce a different shade.
This can reveal problems that are not obvious from the original paint sample.
The recognized ASTM D5326-22 method for color development in tinted latex paints establishes a controlled approach to measuring this type of color difference.
ASTM explains that a conventional finger-rub test can produce substantial variation between operators.
Its standardized approach is designed to improve reproducibility.
The method is specifically intended for tinted latex paints. It should not automatically be described as a validated procedure for every solvent-based coating, industrial coating or other pigment system.
What a Color Difference Means
A coating manufacturer may evaluate the difference between the rubbed and unrubbed areas using instrumental color measurement.
The result can be reported as a color-difference value, often expressed as ΔE under a specified color system.
A larger difference generally indicates a greater change in appearance between the two tested areas.
However, the result does not independently identify the exact cause.
Possible explanations include pigment flocculation, poor colorant compatibility or other forms of pigment separation.
The direction of the color change can also vary.
When a dark colorant becomes better dispersed under shear, the rubbed area may appear darker.
When the white pigment is the less effectively distributed component, the resulting change may follow a different pattern.
The measurement therefore needs to be interpreted alongside the formulation and the actual visual appearance.
A rub-out difference signals investigation, not an automatic rejection of the titanium dioxide supplier.
Flocculation and Pigment Separation Are Related but Different
Coating defects associated with pigment instability can appear in several forms.
Flocculation occurs when dispersed particles form clusters.
Pigment separation occurs when different components in a pigment mixture become unevenly distributed.
In a tinted white coating, titanium dioxide and the colorant may move differently as the film dries.
The result can be visible color variations or a more uniform-looking surface color that changes when a small area is rubbed.
BYK’s technical explanation of floating and rub-up testing describes how different pigment mobilities can affect the final coating appearance.
The guidance also explains that controlled flocculation can sometimes help prevent pigment separation by reducing differences in particle mobility.
That introduces an important technical trade-off.
Complete deflocculation is often desirable in high-gloss coatings where efficient pigment utilization and smooth appearance are priorities.
However, controlled flocculation may be useful in certain systems where suspension stability and resistance to pigment separation are more important.
It can also affect gloss and other properties.
The formulation must therefore be optimized for its intended use rather than based on the assumption that every form of flocculation is equally undesirable.
Why Storage Testing Matters After the Rub-Out Test
A new coating may demonstrate acceptable color development immediately after preparation.
That does not establish that its properties will remain unchanged throughout its intended storage period.
During storage, pigment particles and formulation ingredients continue to interact.
Changes in viscosity, settling, color development or the ease of redispersion may reveal instability.
A useful qualification program should therefore compare the finished coating shortly after manufacture with representative samples after an appropriate storage evaluation.
The test conditions must match the product’s intended handling and storage requirements.
Accelerated storage methods may be useful for screening, but they should not automatically be treated as exact predictions of commercial shelf life.
After storage, the quality team can repeat relevant appearance, viscosity, color-development and application tests.
This helps establish whether an apparent improvement in pigment dispersion continues to provide value once the coating has been stored.
The process is particularly important when changing binders, dispersants or titanium dioxide grades.
Each substitution can affect the balance of the complete formulation.
How Buyers Should Qualify an Alternative Titanium Dioxide Grade
A coating manufacturer should begin with a reference formulation that already meets its technical requirements.
The proposed alternative titanium dioxide can then be evaluated under comparable manufacturing conditions.
The comparison should preserve relevant variables wherever possible, including pigment concentration, binder system, dispersion method and application conditions.
If formulation adjustments are necessary to achieve suitable stability, those changes should be documented.
This prevents the manufacturer from attributing every performance difference to the pigment alone.
The assessment should consider both the raw material and the finished formulation.
For example, a titanium dioxide supplier may report an acceptable particle-size distribution and typical surface-treatment characteristics.
Those results can help establish the material’s identity and technical suitability.
However, they do not demonstrate how it will perform with every customer binder and dispersant.
A certificate of analysis may support lot acceptance for defined pigment properties.
It does not automatically certify finished-paint color development, flocculation resistance or storage stability.
Those characteristics require appropriate application testing.
Compare the Cost of the Finished Coating
A lower-priced titanium dioxide grade may appear commercially attractive.
However, the relevant cost comparison should include any additional dispersant demand, changes in processing time and the ability to achieve the required finished-coating properties.
If a lower-cost pigment requires substantial formulation adjustments or repeatedly fails stability checks, the original purchasing saving may not represent a lower total production cost.
The reverse is also possible.
A less expensive grade may work satisfactorily when combined with an appropriate binder and dispersant system.
This is why formulation-specific qualification matters more than comparing isolated supplier performance claims.
The purchasing decision should reflect the complete coating, not just the price or properties of the pigment powder.
Stable Dispersion Is the Real Performance Target
Titanium dioxide flocculation illustrates why pigment dispersion should be treated as an ongoing formulation requirement rather than a completed grinding step.
A coating may pass its initial fineness check and still experience pigment instability after binder addition or storage.
Rub-out testing can help identify color-development problems in appropriate tinted coatings, while additional stability and application tests provide evidence about the finished product.
Research published in 2026 further demonstrates the trade-offs involved in selecting alternative dispersant and binder systems.
For industrial chemical buyers, the practical conclusion is that a titanium dioxide grade should be qualified under the conditions in which it will actually be used.
A successful grind is the starting point. Consistent coating performance is the real goal.