
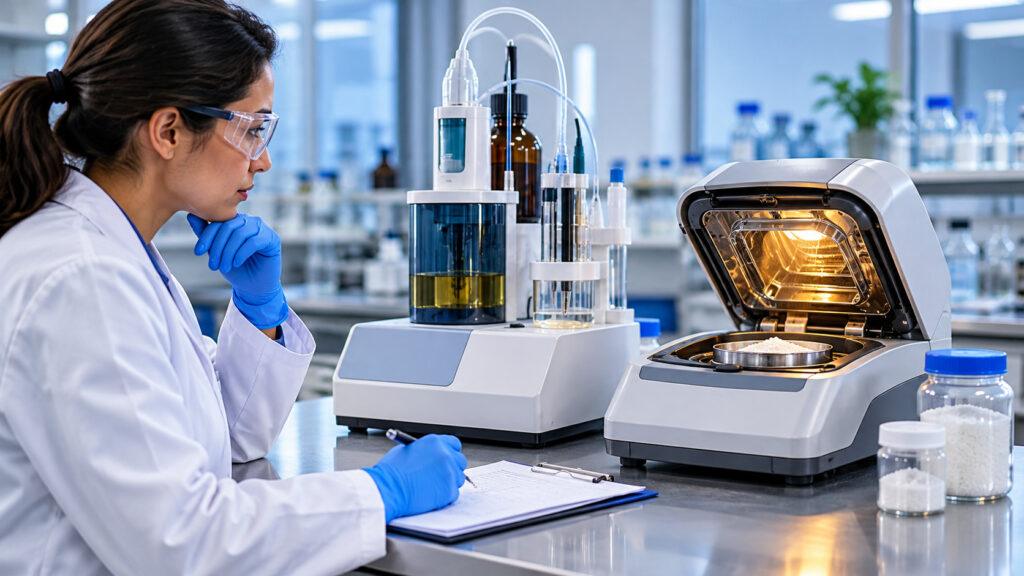
A chemical supplier reports 0.31% moisture by loss on drying, while an independent laboratory measures 0.18% water using Karl Fischer titration. The numbers appear contradictory, but they may both be correct.
The reason is that Karl Fischer titration and loss on drying do not necessarily measure the same property.
Karl Fischer titration determines water through a chemical reaction. Loss on drying measures the mass a sample loses under specified heating conditions, which may include water, residual solvents and other volatile substances.
For industrial chemical buyers, this difference can affect incoming quality inspections, supplier comparisons, material release decisions and production specifications.
A certificate of analysis showing an acceptable moisture percentage is not sufficient unless the reported method measures the property the manufacturing process needs to control.
Water Content and Drying Loss Are Different Measurements
The word “moisture” appears frequently on chemical technical data sheets and certificates of analysis. Unfortunately, it does not always identify the measurement being reported.
A supplier may use the term to describe water content, total volatile loss or another result defined by its internal testing procedure.
These measurements can overlap, but they are not universally equivalent.
What Loss on Drying Measures
Loss on drying, often abbreviated LOD, is based on the reduction in sample mass after controlled heating.
The result depends on several factors, including the material, drying temperature, test duration, sample characteristics and endpoint requirements.
If the sample contains water and another volatile substance, both may contribute to the measured mass loss.
For example, a material containing residual processing solvent may lose some of that solvent during heating.
A laboratory reporting the total mass loss as moisture could therefore overstate the actual water content.
The opposite problem is also possible. Some water may remain in a material because the selected drying conditions do not release it completely.
Heat-sensitive materials can introduce further complications if decomposition or chemical changes affect the measured mass.
These limitations are consistent with the principles of ASTM E1131-25 for thermogravimetric compositional analysis.
That standard covers the measurement of material fractions through mass changes under controlled temperature and atmospheric conditions. It is not a universal loss-on-drying procedure for every industrial chemical, but it illustrates why thermal mass loss must be interpreted in relation to the material and test conditions.
The purchasing implication is straightforward: drying loss should not automatically be reported or interpreted as water content.
What Karl Fischer Titration Measures
Karl Fischer titration uses a chemical reaction involving iodine to determine water.
Unlike a conventional drying-loss measurement, it is intended to quantify water rather than the combined mass of substances that evaporate during heating.
Two principal approaches are used in industrial laboratories: volumetric and coulometric Karl Fischer titration.
Volumetric Karl Fischer Titration
Volumetric Karl Fischer titration determines water from the amount of reagent consumed during the measurement.
The technique can be suitable for a wide range of water concentrations, depending on the material and validated procedure.
The current ASTM E203-24 standard for volumetric Karl Fischer titration describes its application to determining free water and water of hydration in many solid and liquid organic and inorganic substances.
The standard also emphasizes that not every sample can be analyzed directly without addressing possible interference.
This matters when buying materials with complicated chemical compositions.
A material may contain water but also react with the titration reagents, leading to an inaccurate result unless the laboratory has established a suitable method.
Coulometric Karl Fischer Titration
Coulometric Karl Fischer titration generates the iodine required for the reaction electrochemically.
It is especially useful when very small quantities of water need to be measured.
ASTM E203-24 indicates that coulometric determination should be considered when samples routinely contain 500 mg/kg of water or less.
That concentration is equivalent to 0.05% by mass.
For liquid organic chemicals, ASTM E1064-24 covers automated coulometric Karl Fischer determination over a stated range of 0% to 2.0% water by mass.
The method specifically excludes certain liquefied gases, so it should not be applied indiscriminately to every industrial material.
The difference between volumetric and coulometric testing is not simply that one is better.
A laboratory should select the method according to the expected water concentration, chemical composition, potential interference and validated measurement requirements.
A Supplier Comparison Shows Why the Difference Matters
Consider a hypothetical industrial chemical purchased for a moisture-sensitive manufacturing process.
The approved specification establishes a maximum water concentration of 0.25% by mass, determined by a validated Karl Fischer procedure.
The supplier’s certificate of analysis reports:
Moisture: 0.31% by loss on drying
An independent laboratory subsequently measures:
Water: 0.18% by Karl Fischer titration
The numerical difference is:
0.31% − 0.18% = 0.13 percentage points.
Expressed on a mass basis, that difference equals 1,300 mg/kg.
At first glance, the supplier result appears to exceed the 0.25% limit, while the independent result falls below it.
However, these results answer different questions.
The supplier’s measurement reports mass lost during its drying procedure.
The independent laboratory reports water determined through its Karl Fischer method.
If both tests are suitable and correctly performed, the difference could reflect substances other than water leaving the sample during drying.
It could also reflect sample handling, incomplete water release, method interference or differences between the tested samples.
The calculations are illustrative, not actual experimental results.
A purchasing team should not conclude that the supplier’s material passes or fails until it establishes which analytical result is relevant to the contractual specification.
Because the hypothetical limit explicitly requires Karl Fischer testing, the independent water result is more directly relevant to that particular requirement—provided the sample is representative and the method is suitable.
The supplier’s higher drying-loss result may still justify investigation if total volatile content also affects the manufacturing process.
The important lesson is that comparing percentages without checking the measurement basis can produce a false supplier discrepancy.
Karl Fischer Testing Can Also Produce Incorrect Results
Karl Fischer titration is selective for water under suitable conditions, but that does not mean every Karl Fischer measurement is automatically accurate.
Some chemical substances can interfere with the reaction.
Certain aldehydes and ketones, for example, can undergo reactions involving components of conventional Karl Fischer reagents.
Other materials may change the reaction environment, consume reagents or prevent complete water extraction.
Poor sampling can create additional errors.
A hygroscopic powder may absorb atmospheric moisture before analysis. A poorly sealed sample container may allow moisture exchange during transport or storage.
The laboratory must establish whether its procedure is appropriate for the exact material.
Metrohm’s Karl Fischer technical guidance identifies several warning signs of interference or unsuitable testing conditions.
These include unexpected measurement drift, poor reproducibility, incomplete dissolution and results that change with sample quantity.
Metrohm also describes alternative approaches for samples that cannot be analyzed directly.
One option is an oven-based Karl Fischer technique, in which released water is transferred into the measurement cell rather than introducing the sample directly into the reagent.
That arrangement can be useful for certain difficult materials, but it still requires suitable conditions and validation.
The takeaway for quality-control teams is that a method should be selected and demonstrated for the actual chemical matrix rather than accepted solely because it carries a recognized name.
Hydrated Chemicals Need Special Attention
The distinction between free water and chemically associated water becomes especially important when evaluating hydrated salts.
Ferrous sulfate heptahydrate, for example, has the chemical formula FeSO₄·7H₂O and CAS number 7782-63-0.
Its crystalline structure incorporates seven water molecules per formula unit.
That chemically associated water contributes to the compound’s formula mass.
It should not automatically be interpreted as accidental contamination.
An anhydrous material and a hydrated form of the same base compound can therefore have substantially different total water contents even when both meet their respective chemical specifications.
The purchasing requirement must establish whether it concerns surface moisture, free water, water of crystallization, total water under a specified method or another defined property.
Karl Fischer testing may determine water associated with a hydrate when the applicable procedure makes that water available to the reaction. It does not follow that every hydrated material will release all its water under every Karl Fischer procedure.
Heating-based tests can also produce different results depending on whether the conditions release surface moisture, crystal water or decomposition products.
This means a laboratory result cannot establish the hydrate identity or chemical assay on its own.
Suppliers and buyers should verify the chemical formula, grade, assay basis and test method before comparing hydrated and anhydrous materials.
What a Chemical Certificate of Analysis Should Tell Buyers
A certificate of analysis is most useful when it connects a specific production lot to clearly defined acceptance requirements.
For moisture-related measurements, a useful CoA should identify the reported property, result, units, method reference and relevant specification limit.
For example, “Water, Karl Fischer, ASTM E203-24” is more informative than a line labeled simply “Moisture.”
However, identifying a standard does not automatically establish that the laboratory followed it correctly or that the method was appropriate for the material.
The buyer may still need information about sample preparation, analytical validation, reporting conventions and whether the result represents the delivered lot.
The existing guide to supplier certificate of analysis verification explains why reported numerical conformity should be distinguished from independent confirmation of material quality.
Four different documents may be relevant to a purchasing decision.
A certificate of analysis reports selected analytical results associated with a particular lot.
A product specification defines the agreed acceptance requirements, including the required property and method where necessary.
A safety data sheet communicates hazard information and relevant handling precautions. It does not certify water content or product purity.
An independent laboratory report provides evidence for the specific sample and analytical procedures used. Its usefulness depends on sample representativeness and testing quality.
These documents serve related but different purposes.
A buyer should not use an SDS as proof of moisture conformity or treat a single independent result as a universal guarantee of future supplier performance.
Storage Conditions Can Change the Result After Delivery
Even an accurate production-lot measurement does not guarantee that the material’s water content remains unchanged throughout storage.
Moisture-sensitive chemicals can gain water when exposed to humid air.
Other materials may lose water or undergo changes in physical condition under certain storage conditions.
Package integrity, temperature history, repeated opening and sample handling can therefore influence later measurements.
A supplier’s original CoA may accurately describe the tested production lot while no longer reflecting the condition of a partially used container.
The site’s guide to chemical shelf life versus expiration dates explains how storage history and appropriate retesting affect continued material suitability.
For quality teams, an unexpected moisture result should trigger a structured investigation rather than an immediate assumption that the original supplier test was wrong.
The investigation should consider whether the sample represents the delivered material, whether exposure occurred after receipt and whether the same analytical basis was used.
Retesting should be carried out only where appropriate for the chemical and permitted by the applicable quality and safety procedures.
Materials suspected of dangerous decomposition or other instability require qualified EHS assessment before sampling.
Write Moisture Specifications Around the Manufacturing Decision
An effective purchasing specification begins by identifying why the property matters.
If water directly affects a chemical reaction, corrosion risk, product stability or another critical process requirement, a water-specific analytical method may be appropriate.
If the intended control concerns the total amount of volatile material released under defined heating conditions, a drying-loss test may provide more relevant information.
Neither method should be selected merely because it is familiar or produces a favorable number.
The specification should define the measured property, applicable method and edition, reporting units, acceptance limit and any essential sample preparation or reporting requirements.
Where alternate methods are permitted, the buyer and supplier should establish how their results will be compared.
Do not assume that two tests are equivalent because their results are expressed as percentages.
That rule also applies when reviewing historical quality trends. Changing from loss on drying to Karl Fischer testing can shift the reported numerical range without necessarily indicating a change in the material itself.
For industrial chemical procurement, the strongest approval decision connects the analytical method to the intended manufacturing requirement.
A reliable moisture specification is not simply a maximum percentage. It is a clearly defined measurement that both the supplier and the receiving laboratory can reproduce and interpret consistently.